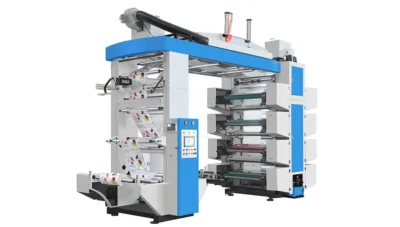
How to Fix Color Misregistration on Your Flexo and Gravure Printing Machines in Nigeria
Running a flexible packaging factory in Lagos, Onitsha, or Kano means constantly working to keep waste margins low. In the Nigerian printing industry, competition is fierce, and customers will not accept bread wrappers, shopping bags, or pure water sachets with blurry text or overlapping colors. When the colors do not line up on the press, you lose expensive polyethylene film and production time. Misregistration rarely shows up as a single dramatic failure; it creeps in — a hairline shift on the third color, a ghosted edge on the second, a register mark that drifts a millimeter more every few hundred meters. That is why it eats so much money before anyone acts. Most of it, though, can be fixed on-site without calling in an outside engineer.
Why the Colors Drift
Registration problems usually come back to how the press handles film tension in West African conditions. PE, PP, and BOPP are sensitive to temperature and to being pulled, and each behaves a little differently: BOPP holds its dimension better than PE, while thin PE stretches more readily under the same tension and heat. If the workshop has no air conditioning, the midday heat plus the hot air from the drying tunnels makes the web stretch between printing stations. Once the film stretches even a millimeter after the first color, the second and third colors will not land where they should.
The register mark is the easiest place to watch this. Print a test run and watch the mark under a strobe light or the press camera: if it drifts steadily in one direction, the web is stretching or the tension is ramping; if it jumps back and forth, look at dust, a loose roller, or mechanical play.
Step 1: Tension and Drying
Start at the unwind and rewind, with the magnetic powder brakes and the automatic tension control. Many factories leave settings on the factory defaults, forgetting that local and imported film batches differ in tensile strength. Set the tension so the web is taut but not so tight that the edges curl inward, and check the result on the printed roll rather than trusting the number on the panel. It also helps to check tension at each station, not just at the unwind: a single over-tight nip or a dragging idler will stretch the web locally and throw off only the colors after it.
Drying is the next place to look. When the tunnels are set hot to force the ink dry faster, the film softens, becomes elastic, and stops registering. Check the temperature in each tunnel zone separately — one zone running hot is enough to soften the web even if the rest look normal. Rather than turning up the heat, raise the exhaust airflow to pull solvent vapor out quickly, so the ink dries at a lower, safer temperature and the web stays stable.
Step 2: Dust and Mechanical Wear
In the dusty Harmattan season, red dust builds up on the idler rollers and plate cylinders and creates friction that jerks the film as it passes each color station. The rollers that matter most are the ones between color stations and at the infeed — those set the path the web follows, so a build-up there shows up directly as registration drift. Clean them daily, with a soft brush rather than solvent on rubber-covered rollers, but stop the press, lock out the power, and wait for the rollers to come to a full stop before you reach in. Never wipe a running press; the in-running nip will pull a hand in.
Finally, check the mechanical wear. Gears and bearings on an older stack press develop play or backlash after months of running on generator power. Check the plate cylinder gears for wear, feel for backlash by rocking the gear by hand with the press locked out, and re-lubricate the gear train. Lock the doctor blade assembly tight as well — a blade that shifts slightly changes the ink film on the plate and shows up as a colour that never quite settles. That small vibration is what makes colors dance at speed.
Registration is mostly a tension-and-temperature problem, with dust and wear adding their share. Fix the web, the drying balance, the rollers, and the gear train in that order, and watch the register mark after each change so you know what actually helped. Startup waste usually drops noticeably.
If your plant keeps chasing registration on a flexo or gravure press, or you are comparing presses built for humid, dusty conditions, our technical team would be glad to review your setup.